Multi-functional Distiller
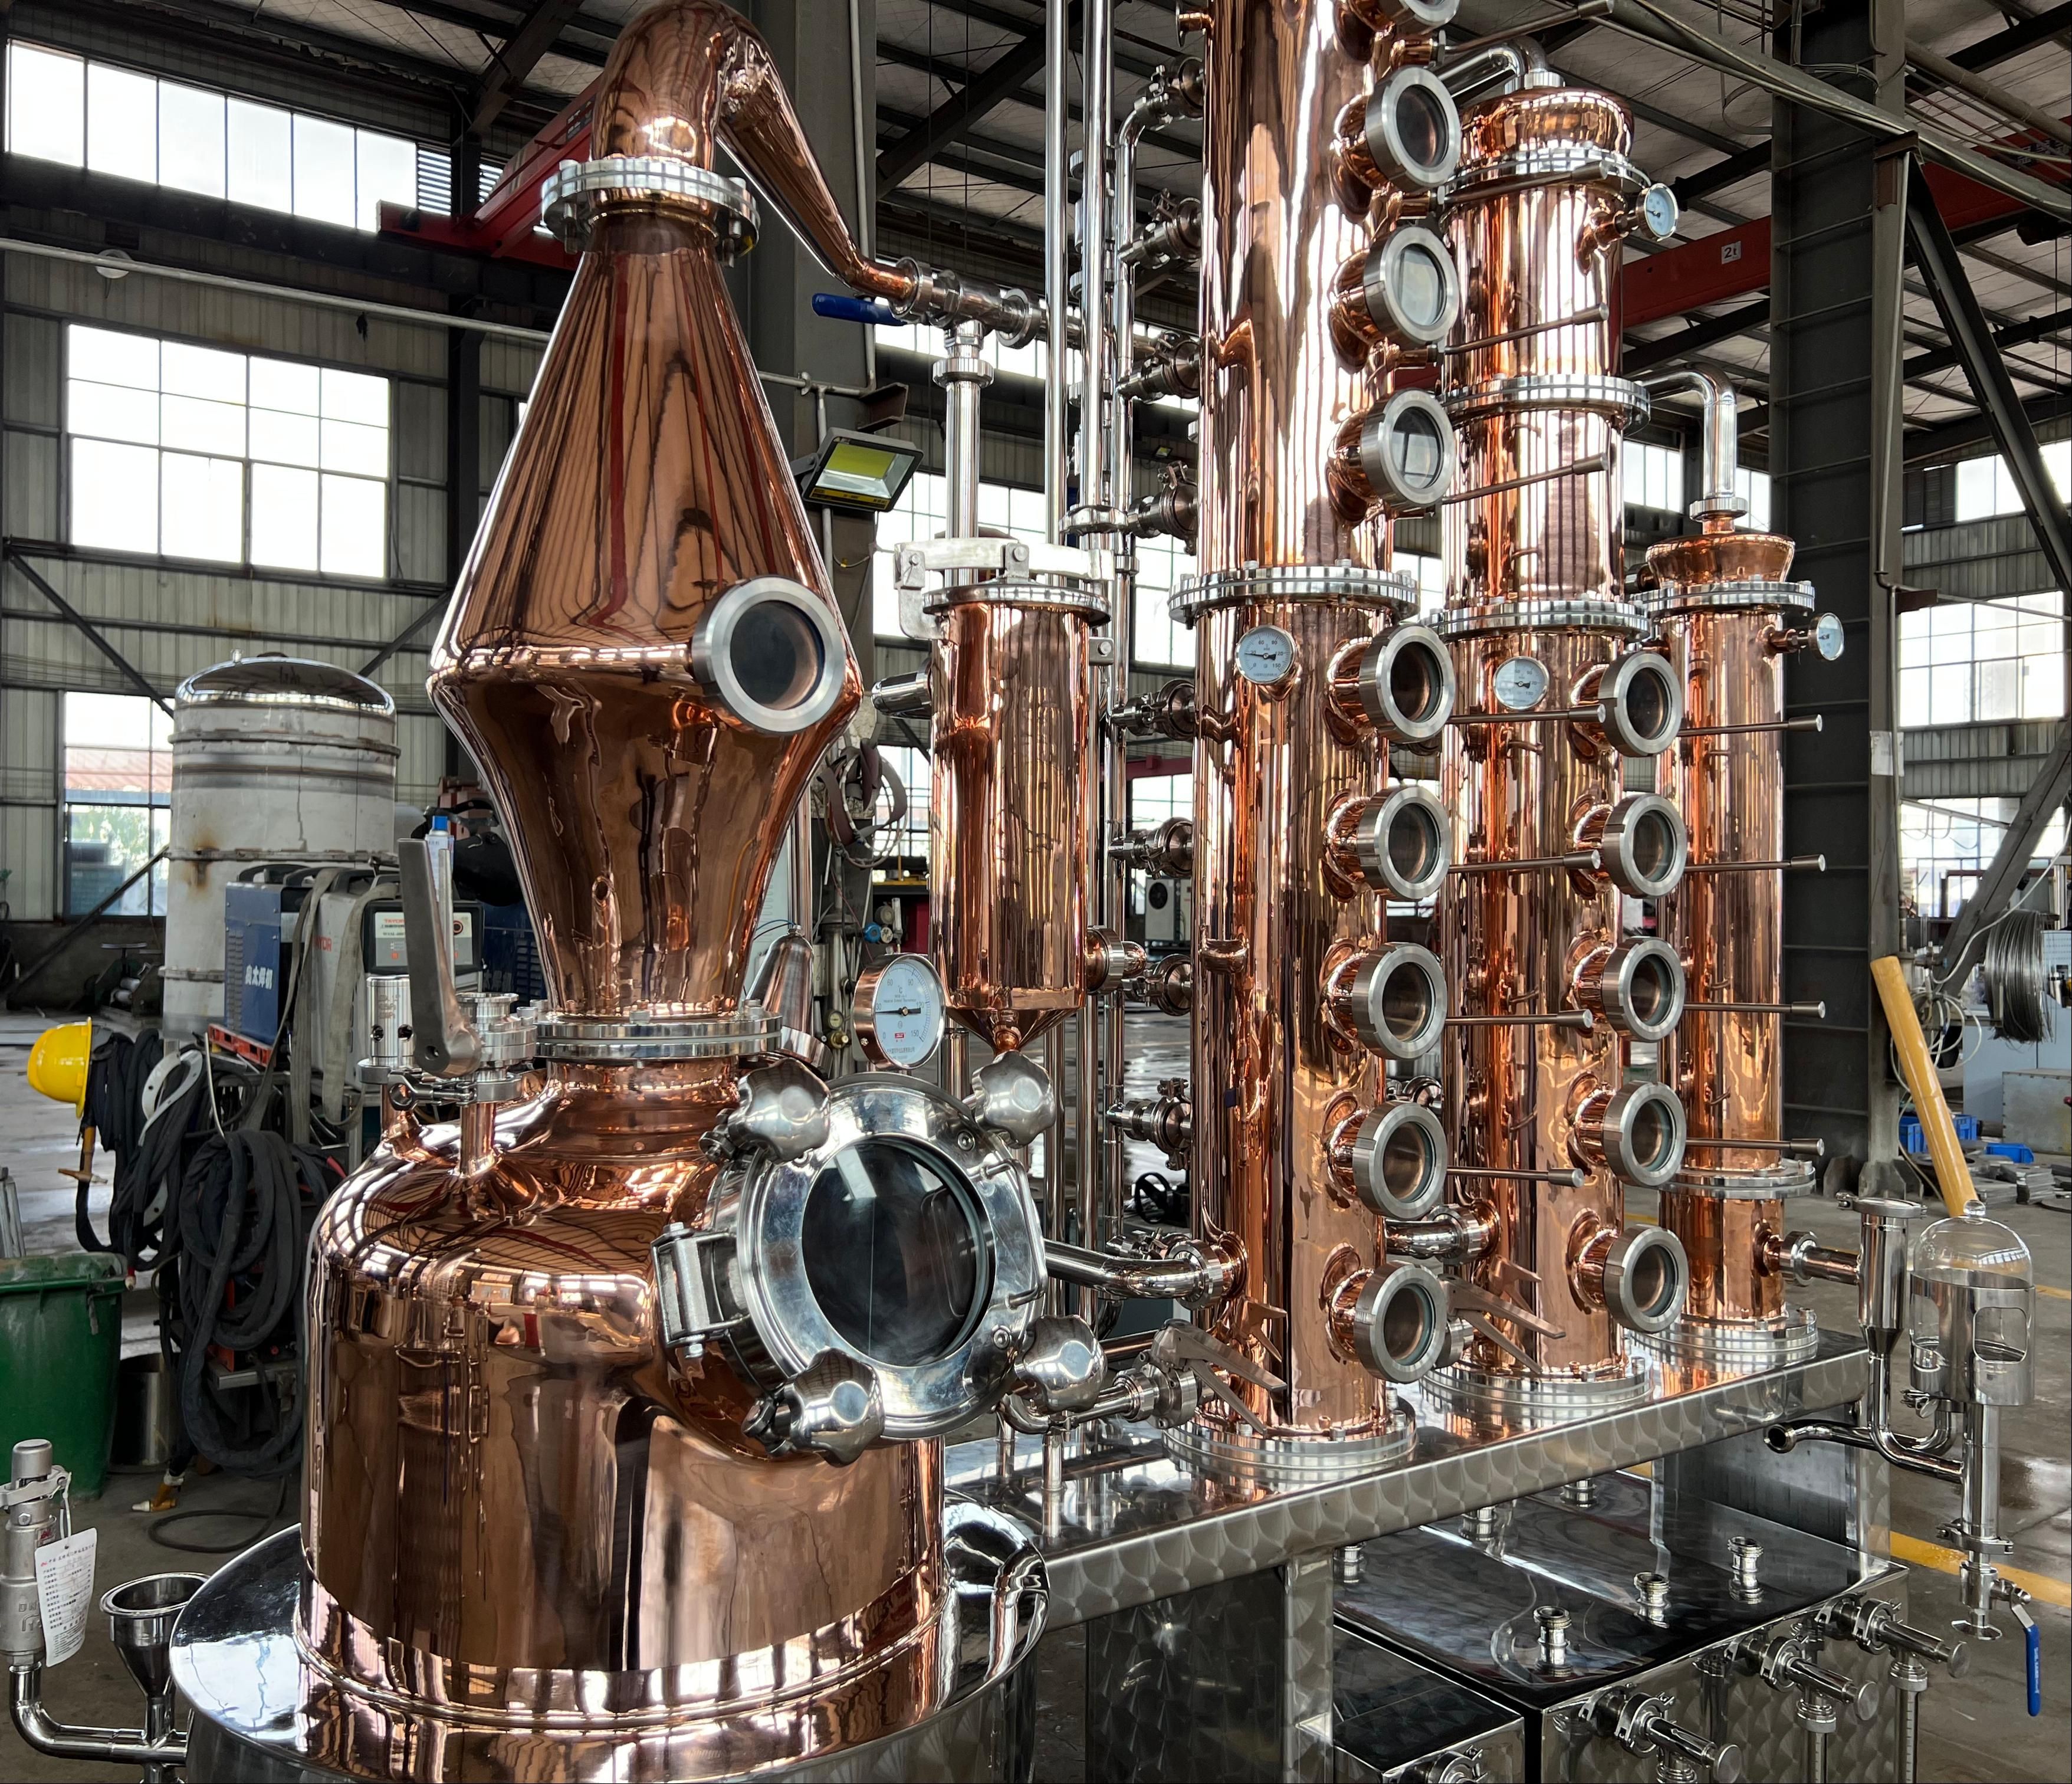
Professional Precision for Craft Spirits and Extracts
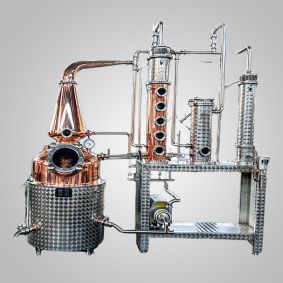
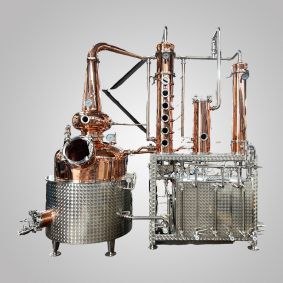
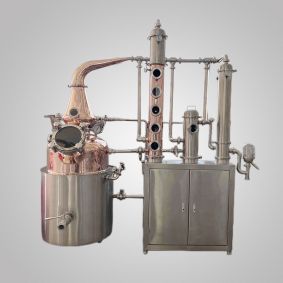
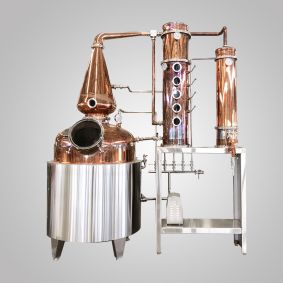
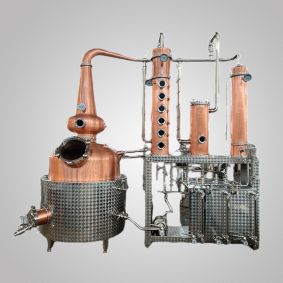
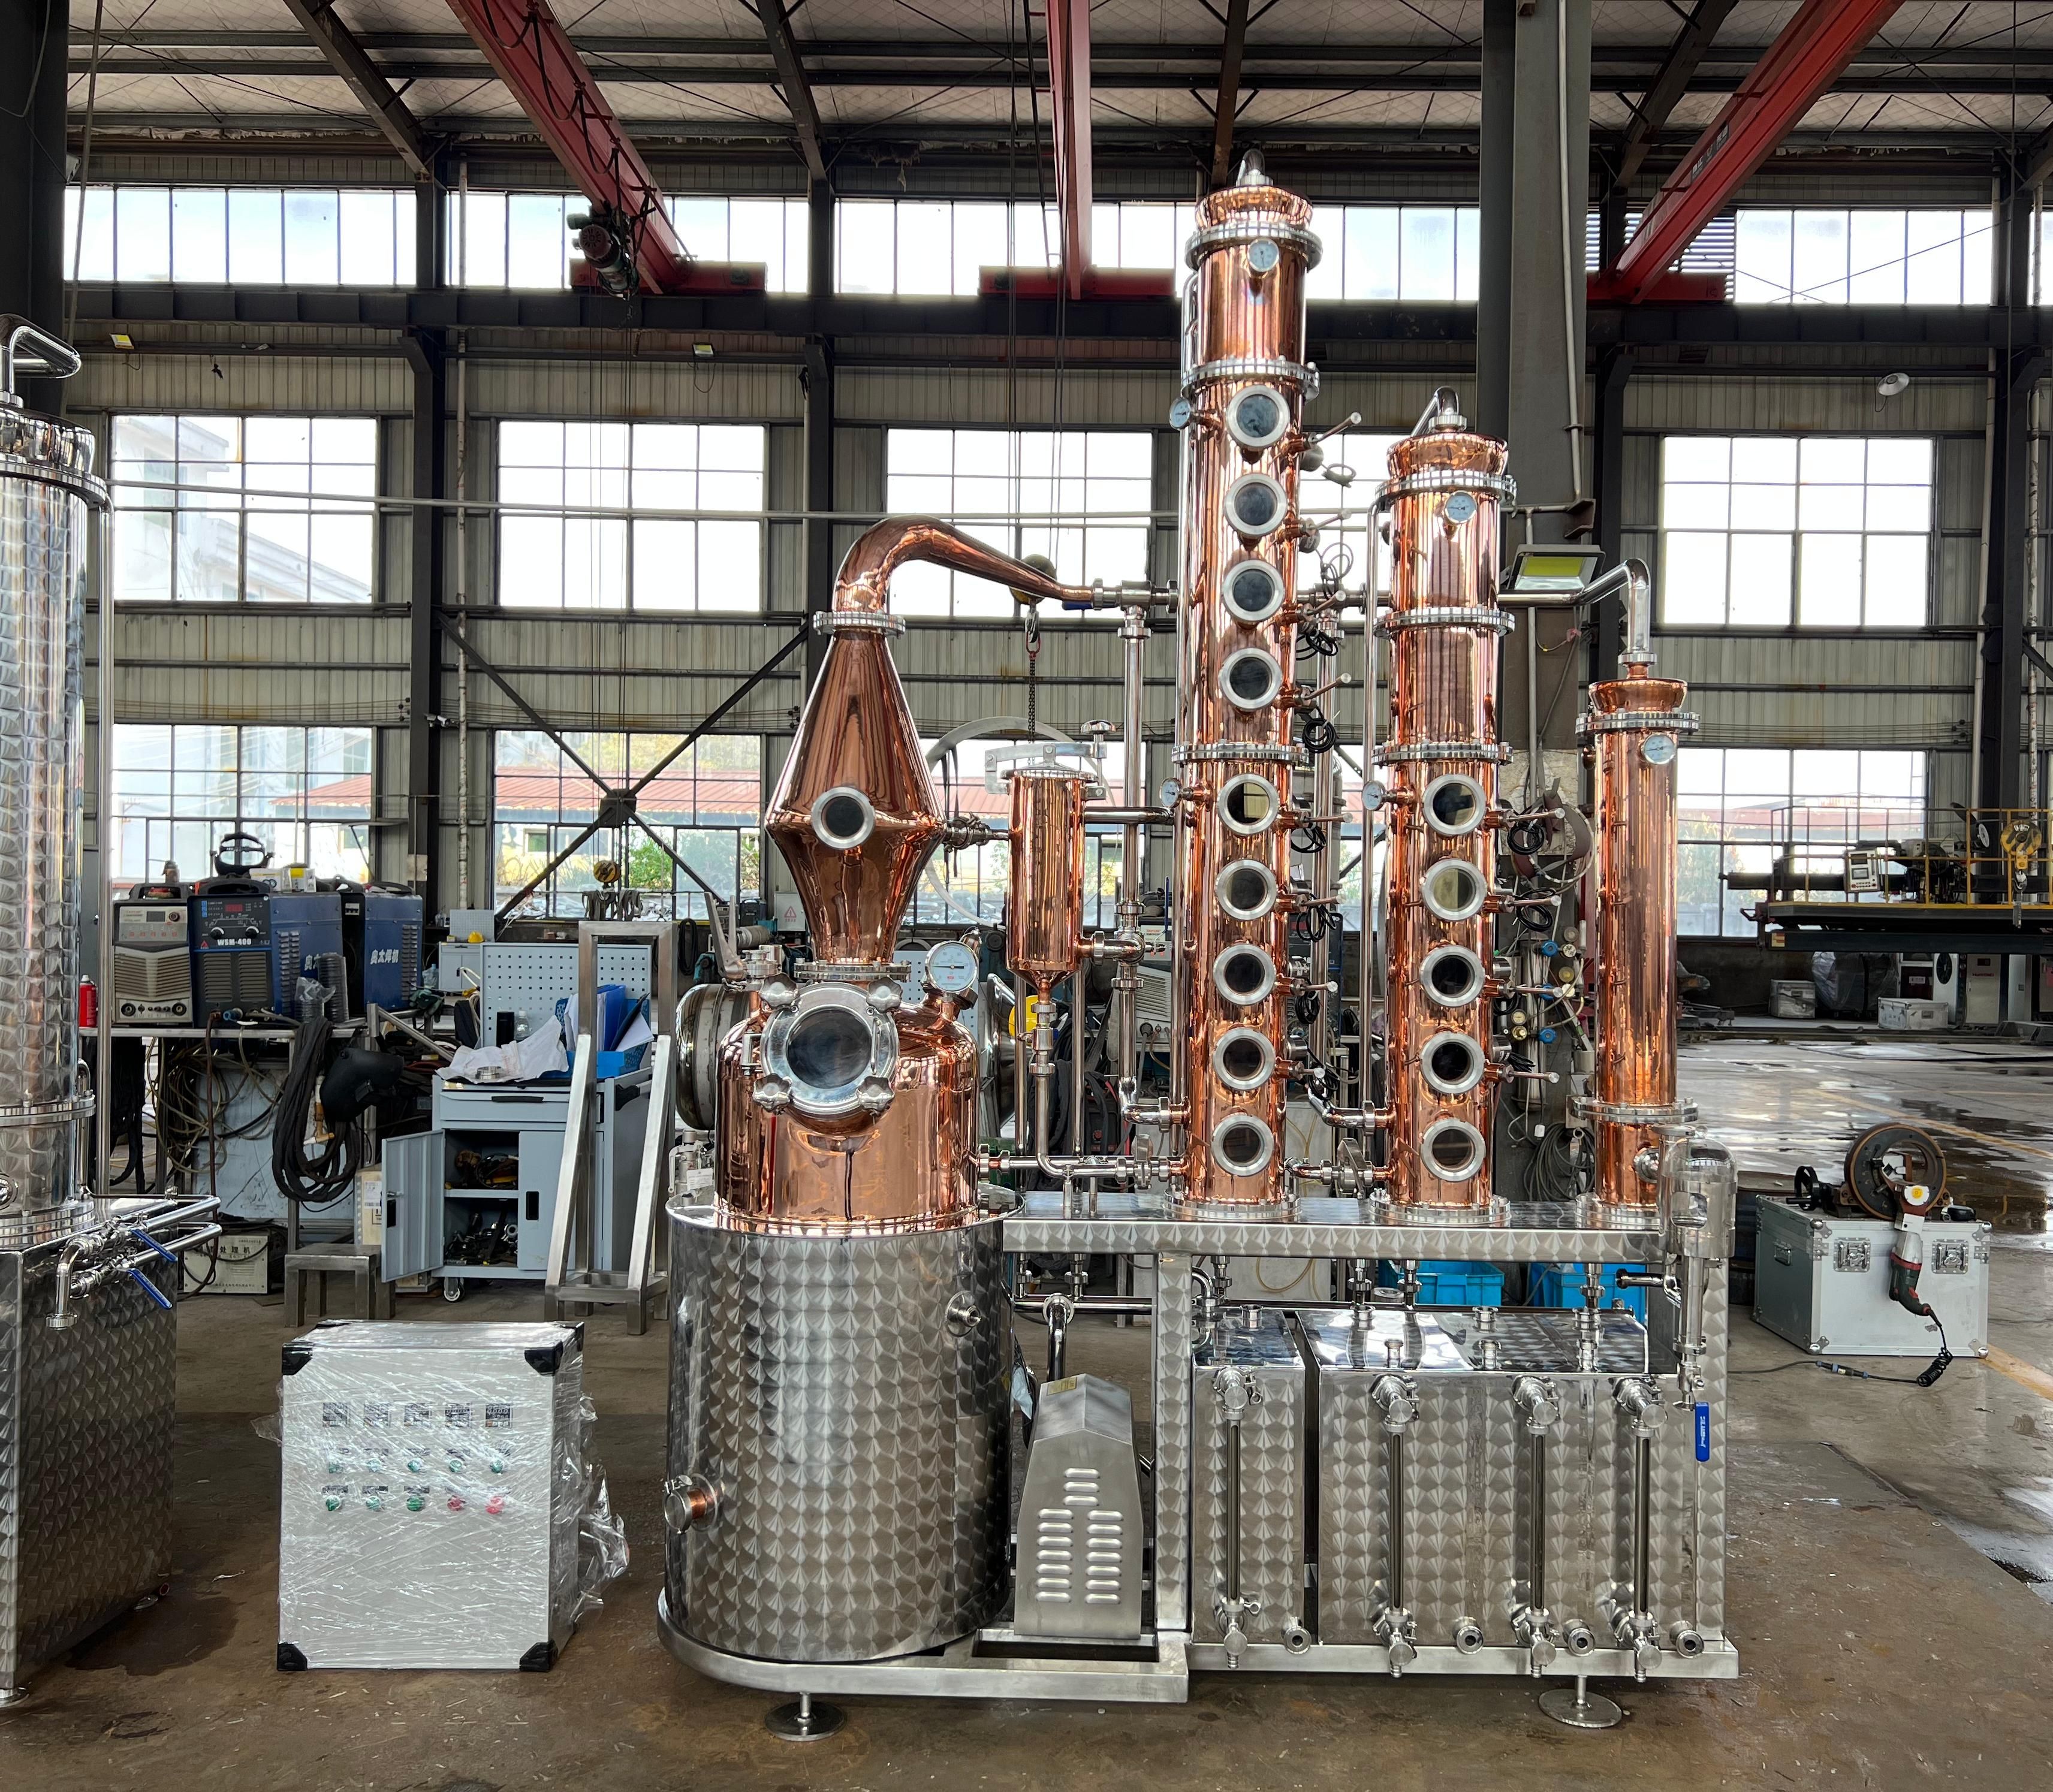
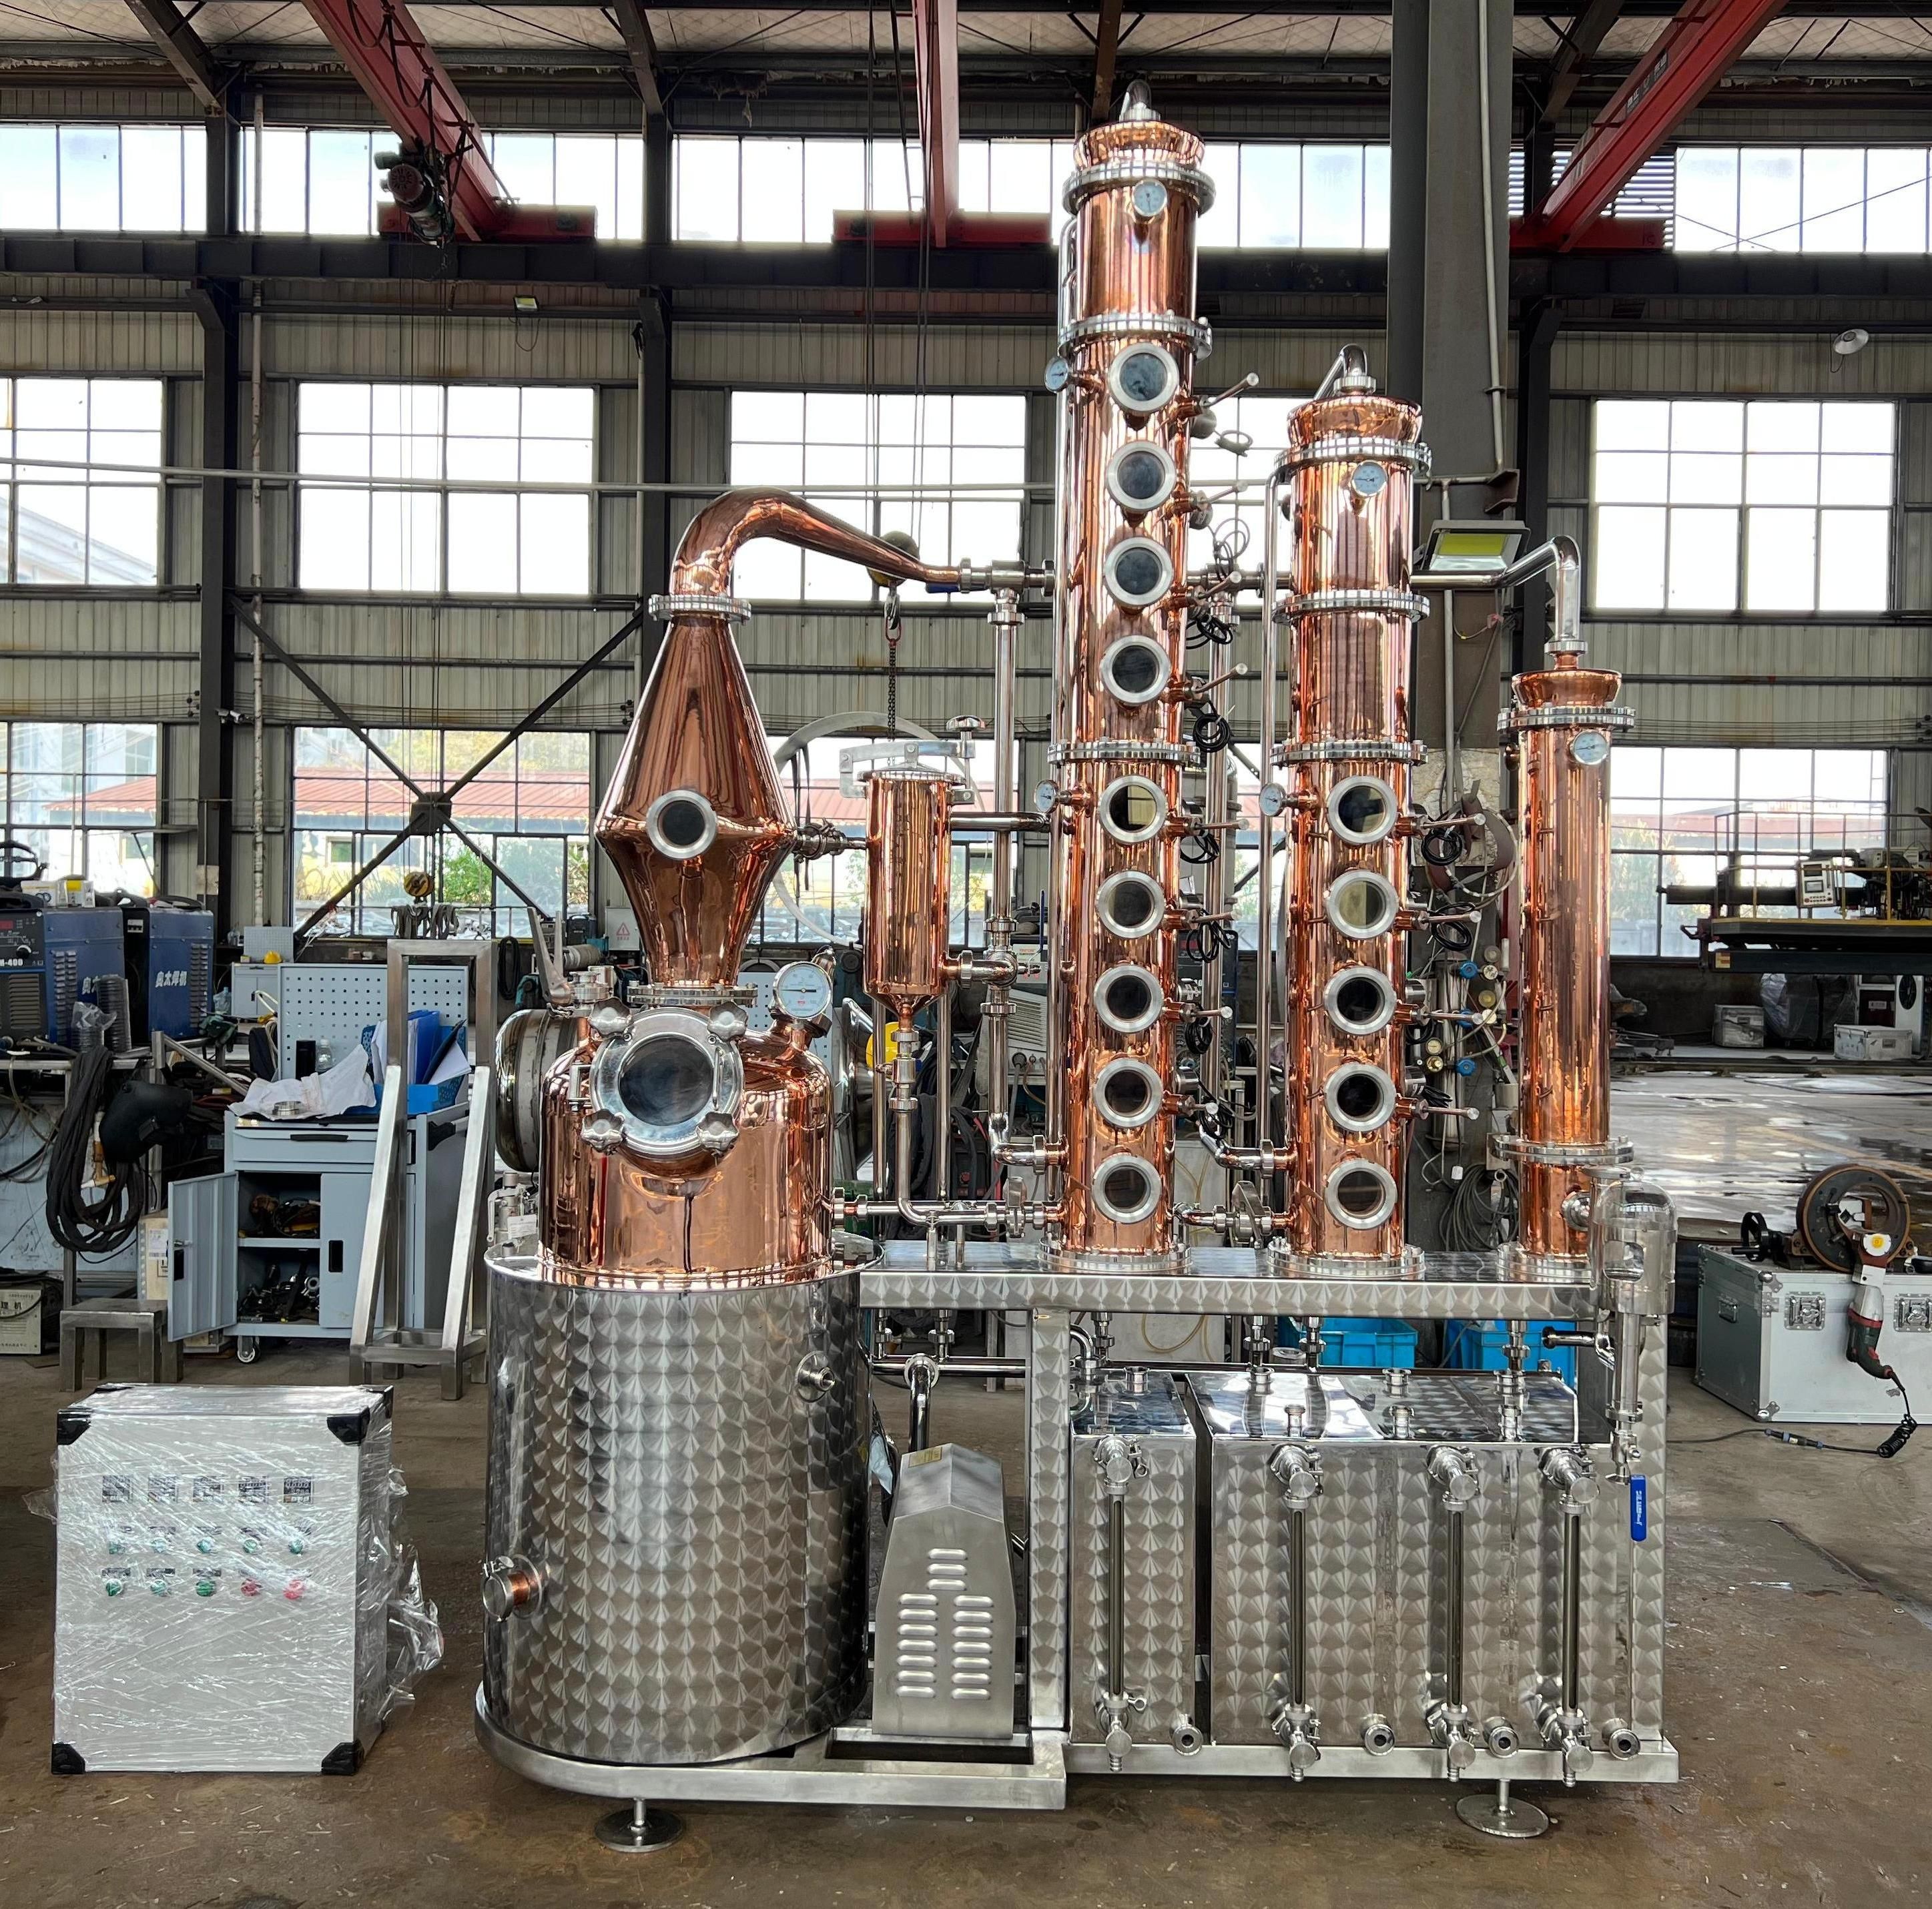
The 100L Multi-purpose Distillation System is a comprehensive, high-capacity unit designed to meet the rigorous demands of professional distilleries and extraction labs. Engineered for both versatility and performance, the 100L Multi-purpose Distillation System seamlessly integrates traditional copper pot still functionality with advanced rectification technology.
Premium Copper and Stainless Steel Construction
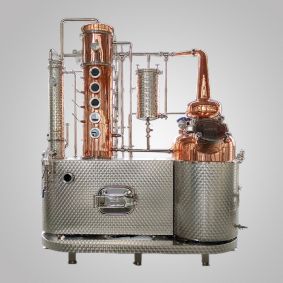
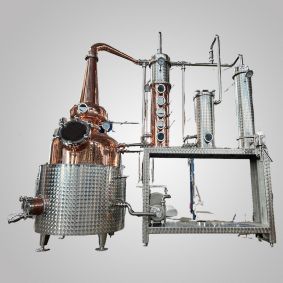
The 100L Multi purpose Distillation System features a hybrid construction that maximizes both quality and durability. The upper boiler and all rectification columns are crafted from high-purity copper to facilitate natural catalysis and remove unwanted sulfur compounds. The boiler’s base and the entire supporting frame are made from food-grade 304/316 stainless steel with a polished diamond-pattern finish, ensuring the 100L Multi purpose Distillation System is as hygienic as it is visually striking.
Advanced Multi-Column Rectification
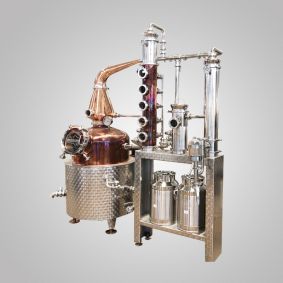
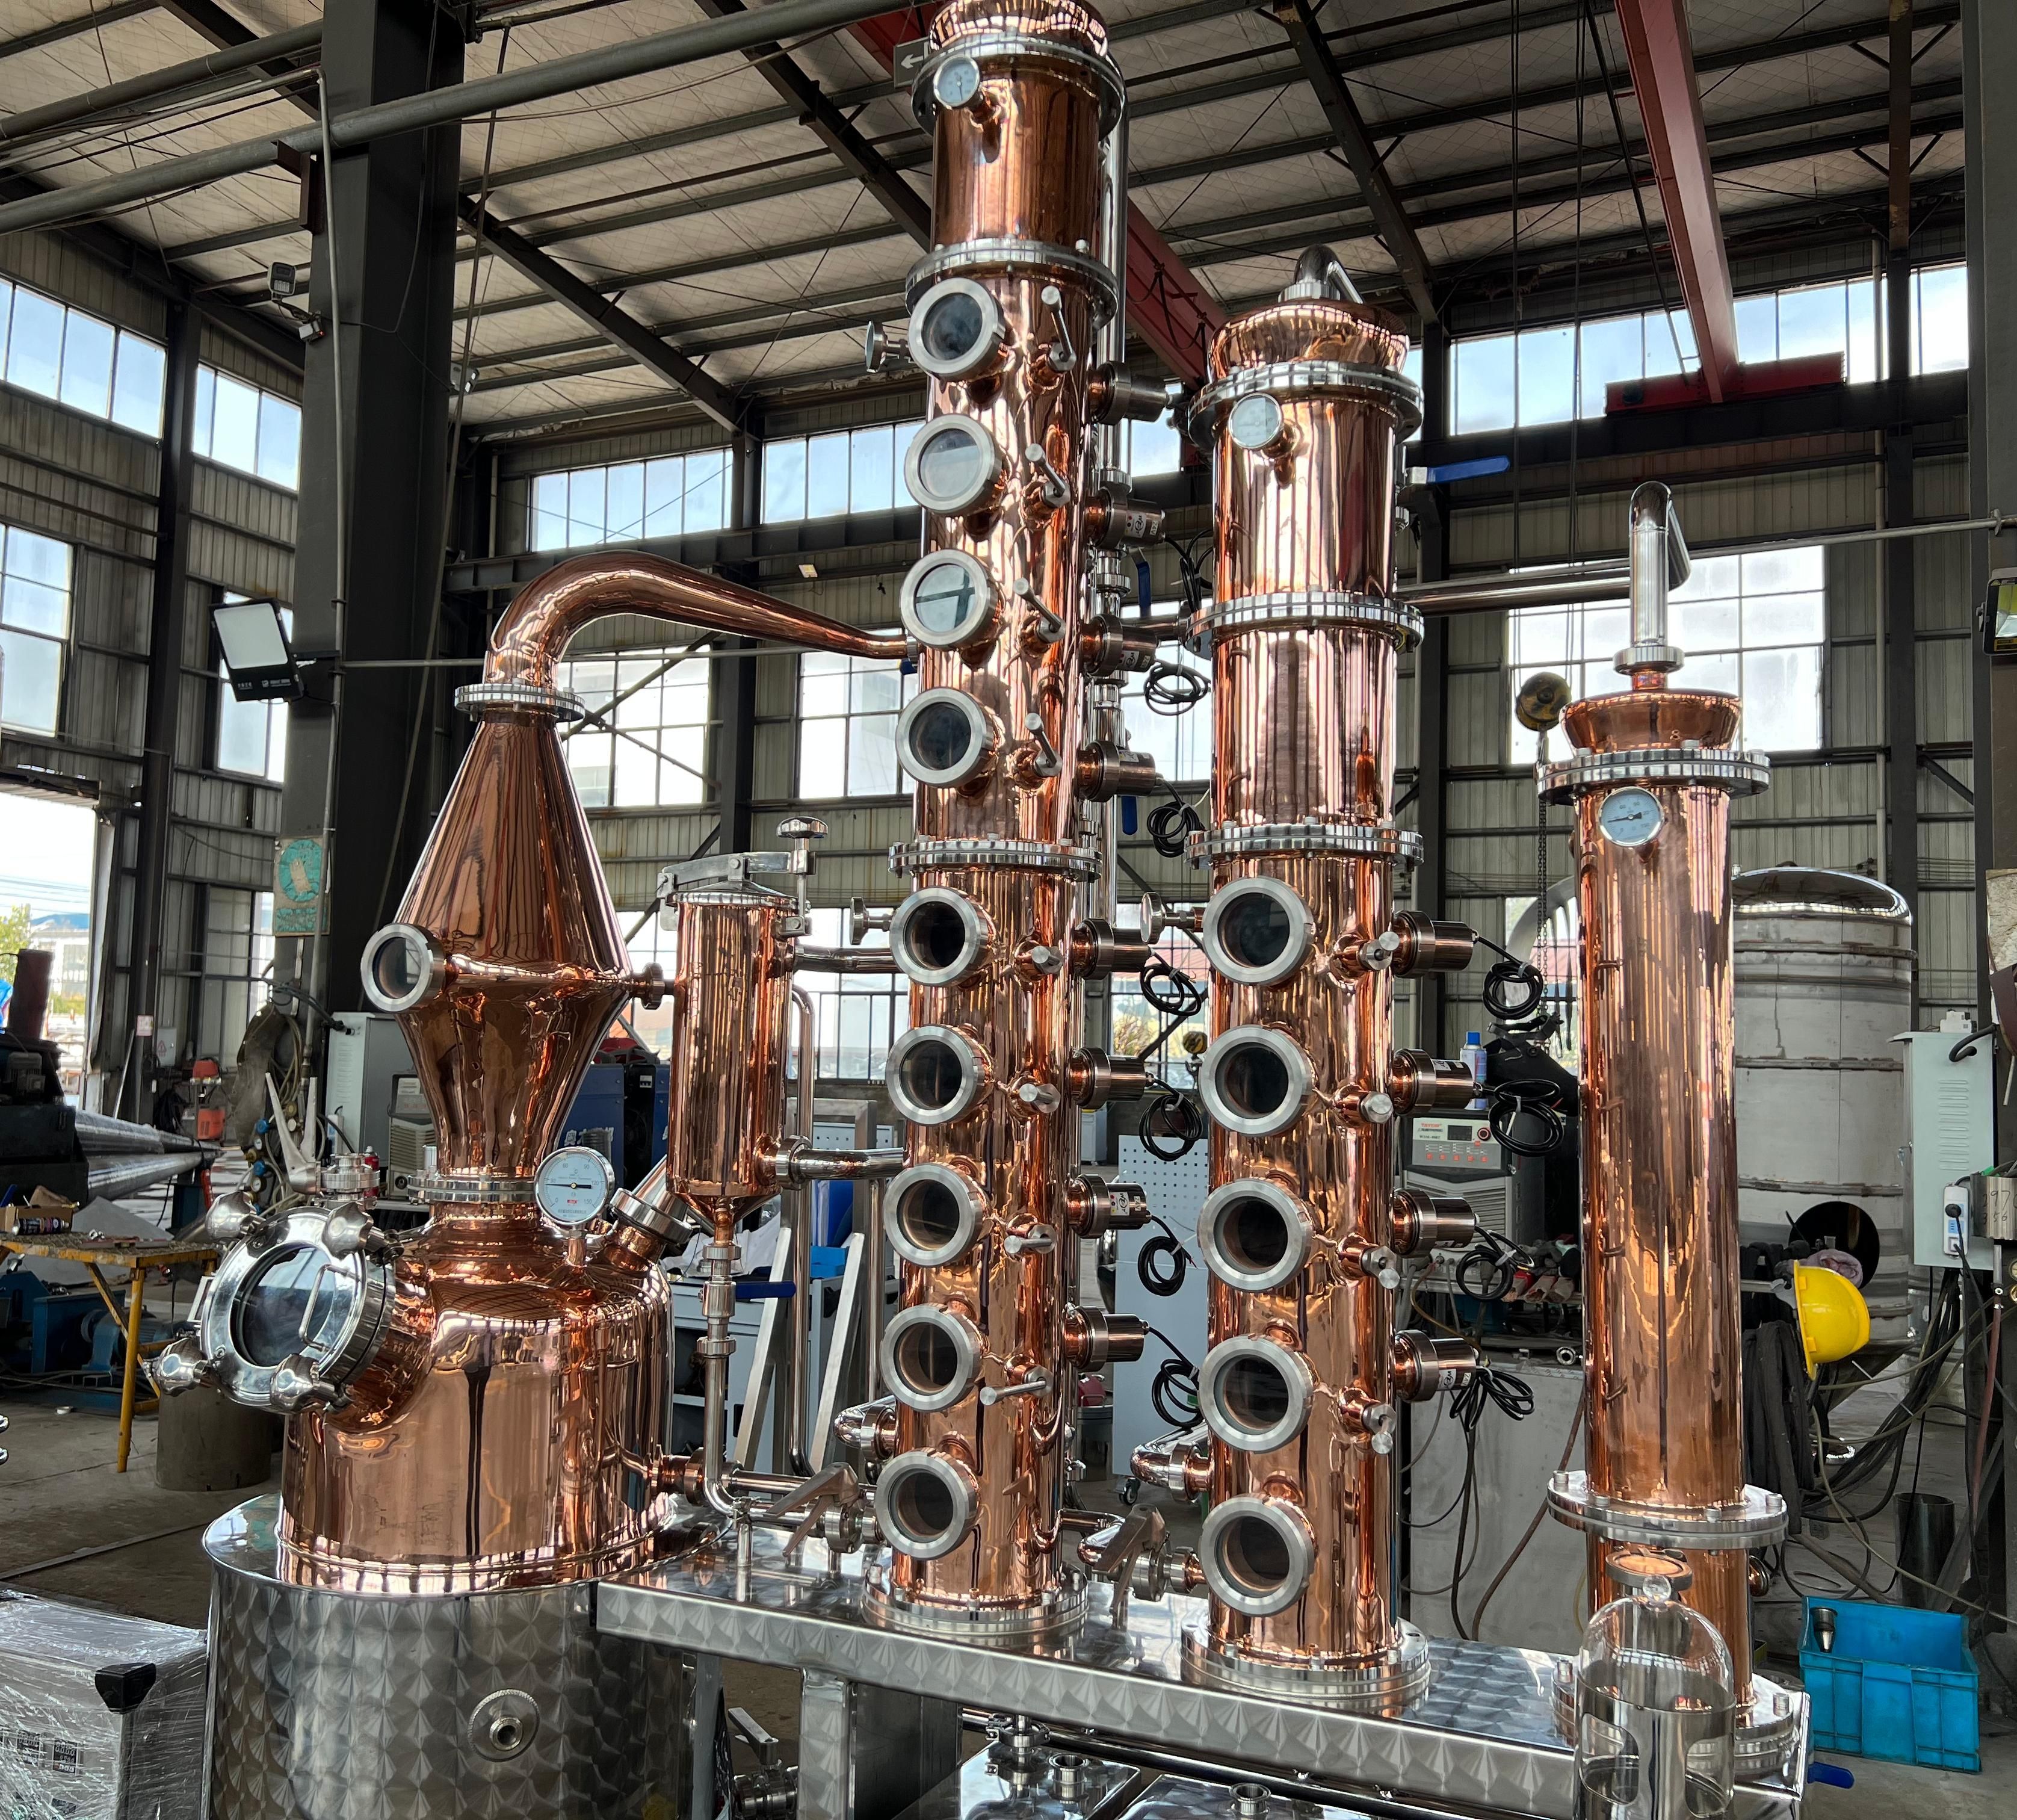
What sets the 100L Multi purpose Distillation System apart is its dual-column architecture. The primary rectification column features 8–10 theoretical plates, each fitted with a large sight glass. This allows the operator to observe the liquid-vapor balance at every stage. A secondary copper column provides additional purification or flavor retention, making the 100L Multi purpose Distillation System truly "multi-purpose"—capable of producing everything from high-proof neutral spirits to complex, flavorful botanicals.
Integrated Modular Design
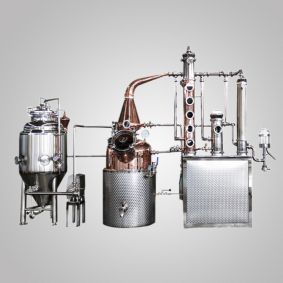
The 100L Multi purpose Distillation System is designed as a self-contained workstation. It includes:
- Dual Collection Vessels: Integrated into the frame for efficient "heads, hearts, and tails" separation.
- Integrated Control Panel: A dedicated electrical station manages heating elements and system
parameters with precision.
- Strategic Visibility: With over ten sight glasses across the boiler, columns, and collection points, the 100L Multi purpose Distillation System offers complete visual oversight of the process from start to finish.
ZR BREW is a leading manufacturer of brewing, distilling, winemaking, and kombucha fermentation equipment with 14 years of industry expertise. We are dedicated to our high-end product line and uphold the craftsman spirit to deliver first-class brewing solutions. With a strong reputation for quality and reliability, we have established partnerships with clients across more than 40 countries worldwide.
Application | Use Case |
Spirits | Whiskey, brandy, gin, vodka, rum |
Botanical Extracts | Essential oils, herbal distillates |
Purified Water | Distilled / deionized water production |
R&D / Education | Lab-scale distillation experiments & training |
| Model | ZR-DT-100L |
| Capacity | Effective volume: 100L |
| Material | SUS304 SUS316 Red Copper |
| Uasge | Whisky Brandy Rum Gin Vodka Others |
| Application | Home commercial |
| Heating way | Electric heating Steam heating Direct fire heating |
| Control System | Fully automated with PLC Siemens Semi-Automated with PID Schneider |
| Voltage | Three-phase/380(220, 415,480…)v/50(60)Hz Single phase/220(110, 240…)v/50(60)Hz |
| Note:1Barrel (BBL) =117 Liter 1Hl=100 Liter 1Gallon=3.7854 Liter | |
| Types | Volume | Component |
| Whisky distiller | 50-5000L | Still pot, swan neck, condenser, CIP, pipe system |
| Vodka distiller | 50-5000L | Still pot , onion head, column, dephlegmator, condenser, pipe system |
| Brandy distiller | 50-5000L | Still pot, onion head, dephlegmator, column, condenser ,CIP, pipe system |
| Rum distiller | 50-5000L | Still pot, column, condenser, CIP, pipe system |
| Gin distiller | 50-5000L | Still pot, column, gin basket, condenser, CIP, pipe system |
| Multi-spirits distiller | 200-5000L | Still pot, onion head, dephlegmator, column, gin basket, condenser, CIP, collecting tank |
1. Material & Craftsmanship
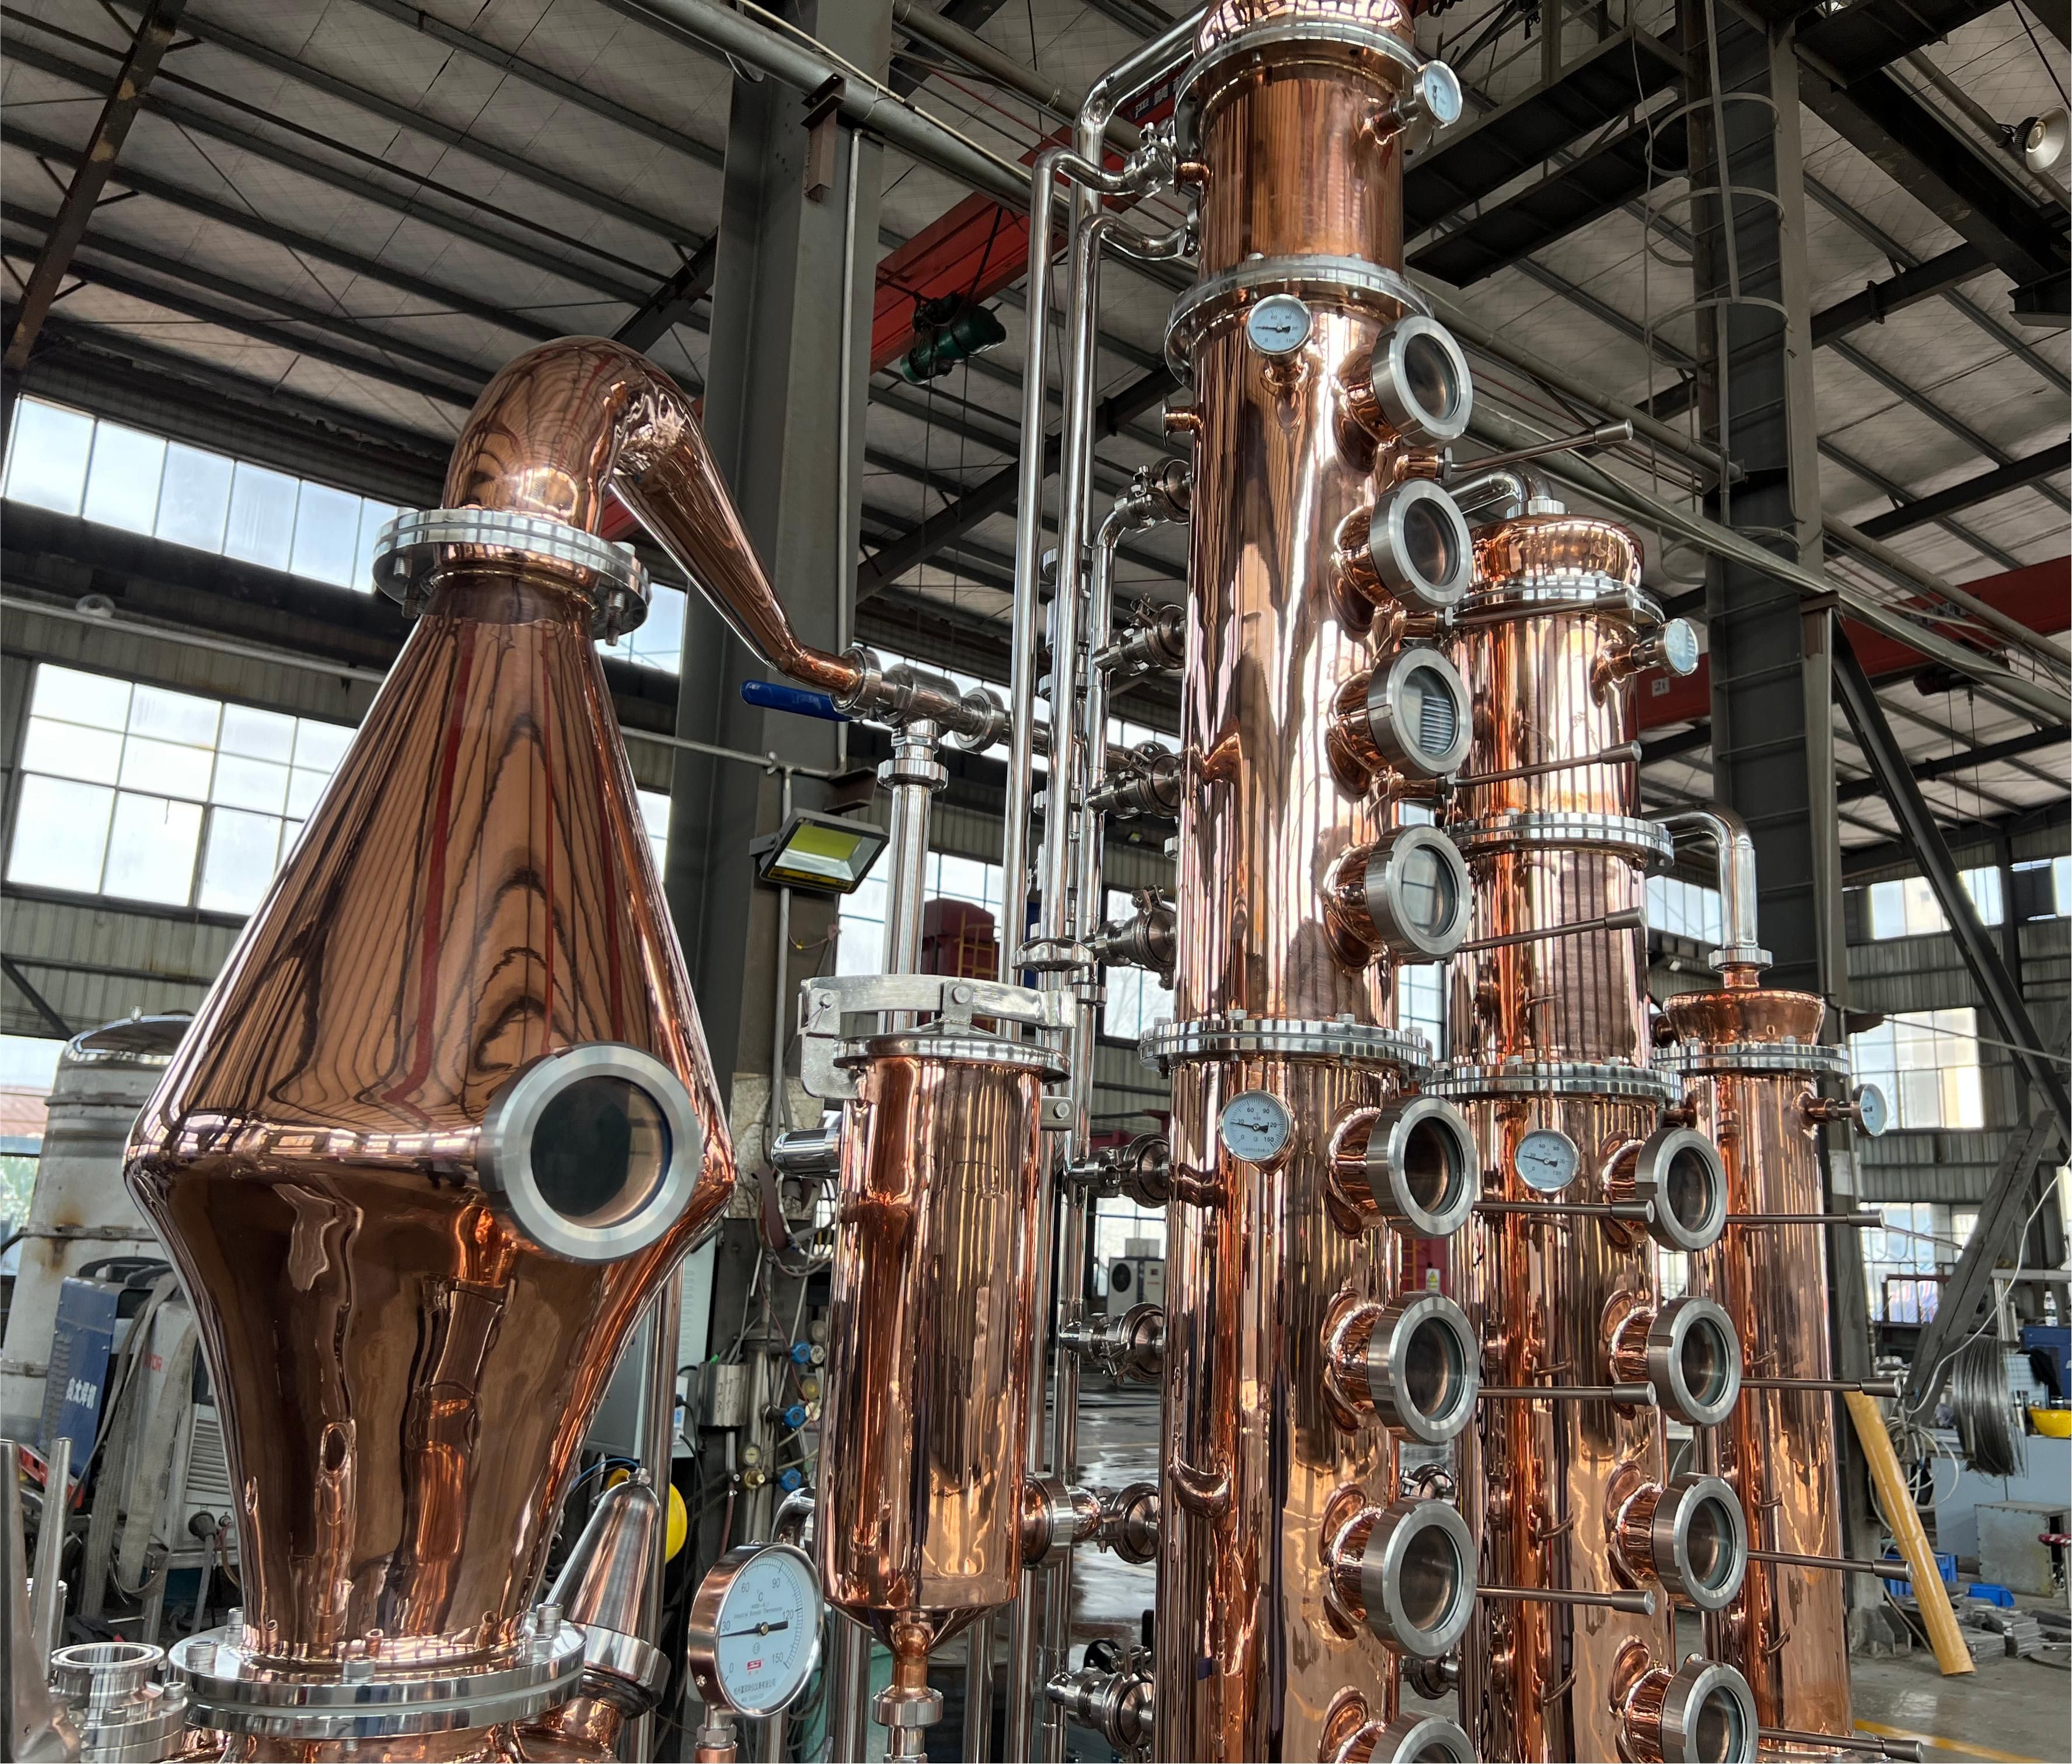
• Full Copper Contact Pathway: Pot boiler, conical helmet, lyne arm, rectification columns, and condenser all crafted from premium red copper. Copper actively reacts with sulfur compounds during distillation, eliminating off-odors and delivering exceptionally pure, smooth tasting spirits.
• 304 Stainless Steel Frame & Base: Hammered-finish stainless steel boiler jacket and structural frame provide superior durability, food-grade hygiene compliance, and a striking professional appearance.
• Sanitary Tri-Clamp Connections: Every pipeline junction uses quick-clamp ferrule fittings for tool-free disassembly, thorough cleaning, and zero dead corners — ensuring full compliance with international food-safety standards.
2. Functional Design
• High-Plate Rectification Column: Equipped with 8+ copper distillation plates across multiple column sections. Each plate features an observation sight glass for real-time reflux monitoring and precise fraction separation control.
• Dedicated Gin Botanics Basket: Separate column section allows vapor-path infusion of botanicals, enabling gin production without cross-contamination from other spirit runs.
• Multi-Purpose Versatility: Suitable for distilling Whiskey, Brandy, Rum, Gin, Vodka, Absinthe, and other spirits. One unit replaces multiple dedicated stills for diverse craft distillery production needs.
• Dual Collection Vessel System: Multiple stainless steel receiving containers with independent take-off valves enable simultaneous heads/hearts/tails separation for uninterrupted production runs.
3. Temperature Control & Monitoring
• Multi-Point Pressure Gauges: Industrial-grade pressure indicators installed at the pot, each column section, and condenser for real-time safety monitoring across the entire system.
• Precision Temperature Detection: Thermometer ports at critical process points allow operators to monitor vapor temperature at each plate stage, ensuring consistent distillation accuracy and batch-to-batch quality.
• Electric Heating Control Panel: Dedicated stainless steel control cabinet with individual heating zone switches, power indicators, and emergency safety alarms for precise thermal management.
4. Structural Advantages
• Integrated Skid-Mounted Design: All components — boiler, columns, condenser, collection vessels, and controls — pre-assembled on a single heavy-duty stainless steel frame. Compact footprint with minimal on-site installation required.
• Modular Column Architecture: Each column section is independently removable via tri-clamp connections, allowing operators to configure the system for different products, adjust plate counts, or bypass sections as needed.
• Decorative Copper Helmet Design: The distinctive conical helmet shape not only provides authentic pot-still character but also serves as a visual centerpiece for visitor-facing distillery showrooms and tasting rooms.
• Professional-Grade Construction: Mirror-polished copper surfaces, precision-welded joints, and industrial-quality fittings ensure reliable long-term commercial operation with minimal maintenance downtime.
What is the capacity of the 100L Multifunctional Distillation System?
The 100L Multifunctional Distillation System features a 100-liter boiler capacity. With the recommended 50-60% fill rate, you can process 50-60L of mash per batch, yielding approximately 10-15L of high-proof spirit per run.
What heating options are available for the 100L Multifunctional Distillation System?
The 100L Multifunctional Distillation System offers multiple heating options: - Electric heating (recommended): 12-18 kW with digital temperature control - Gas/diesel burner - Steam heating The control panel allows easy temperature monitoring and adjustment for precise distillation control.
How much spirit can the 100L Multifunctional Distillation System produce per batch?
The 100L Multifunctional Distillation System produces approximately 10-15L of 90-95% ABV neutral spirit per 100L wash. For flavored spirits like whiskey or brandy, yield may vary based on your recipe and desired proof. Q: How long does one distillation cycle take with the 100L Multifunctional Distillation System?
Is the 100L Multifunctional Distillation System easy to operate?
Yes. The 100L Multifunctional Distillation System is designed for user-friendly operation: - Intuitive control panel with temperature display - Sight glasses on all columns for visual monitoring - Manual valves for easy flow control - Complete operation manual and video tutorials included - No specialized training required for basic operation
Can I customize the configuration of the 100L Multifunctional Distillation System?
Yes. The 100L Multifunctional Distillation System can be customized to meet your specific needs: - Column height and number of plates - Heating method (electric/gas/steam) - Voltage and frequency (110V/220V/380V, 50/60Hz) - Copper or stainless steel columns - Additional safety features - Custom color and finish - PLC control system upgrade
Shandong Zeren Machinery Equipment Co., Ltd. is an equipment manufacturer focusing on biological fermentation industry
Copyright © Shandong Zeren Machinery Equipment Co., Ltd. All Rights Reserved |
Sitemap
| Technical Support: