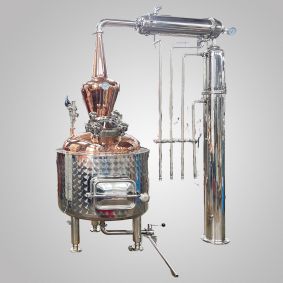
Whiskey Column Still Distiller
Professional-Grade Precision for Craft Whiskey
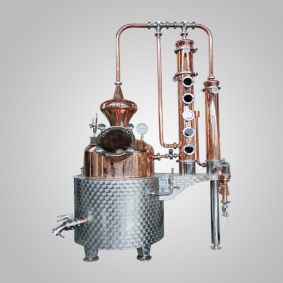
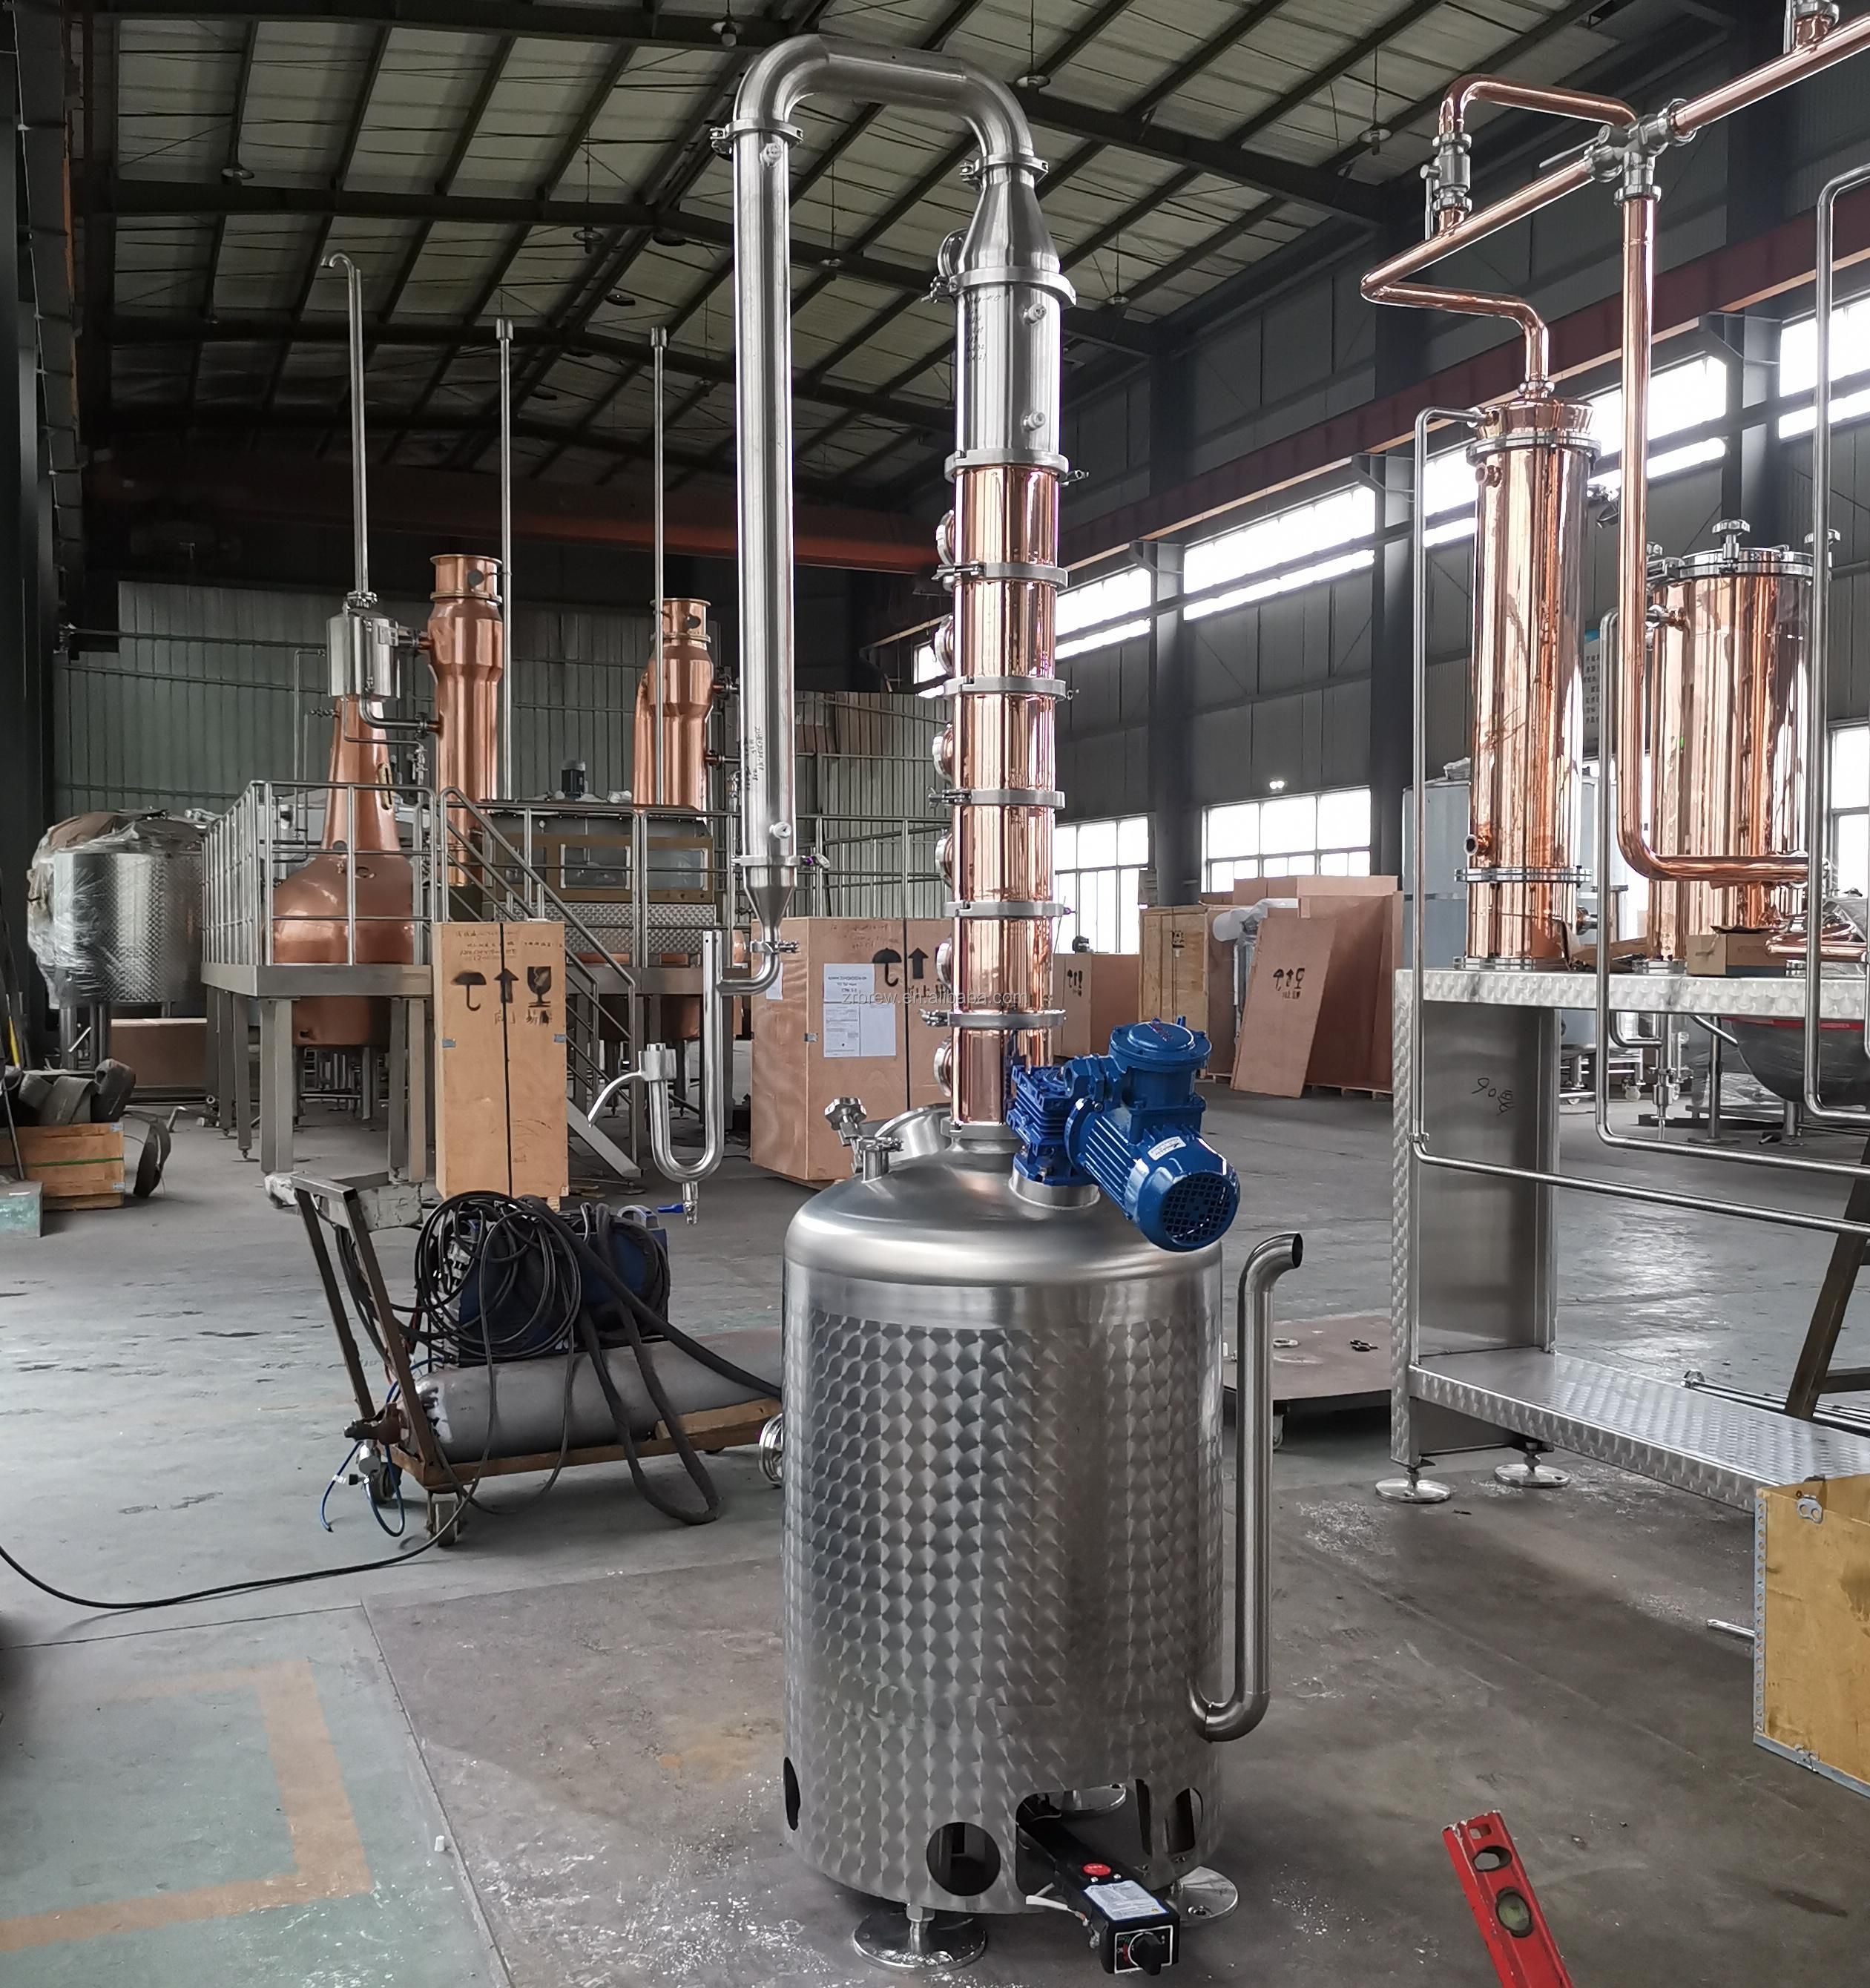
The 100L Column Still for Whiskey Distillation is a comprehensive, professional-grade unit engineered specifically for craft distilleries dedicated to premium whiskey production. Featuring a direct fire heating system, it perfectly combines traditional copper distillation advantages with modern column distilling technology. This still delivers consistent, high-quality whiskey with rich flavor and a clean profile, and it is also highly suitable for bourbon, rum, and brandy making.
Direct Fire Heating & Premium Construction
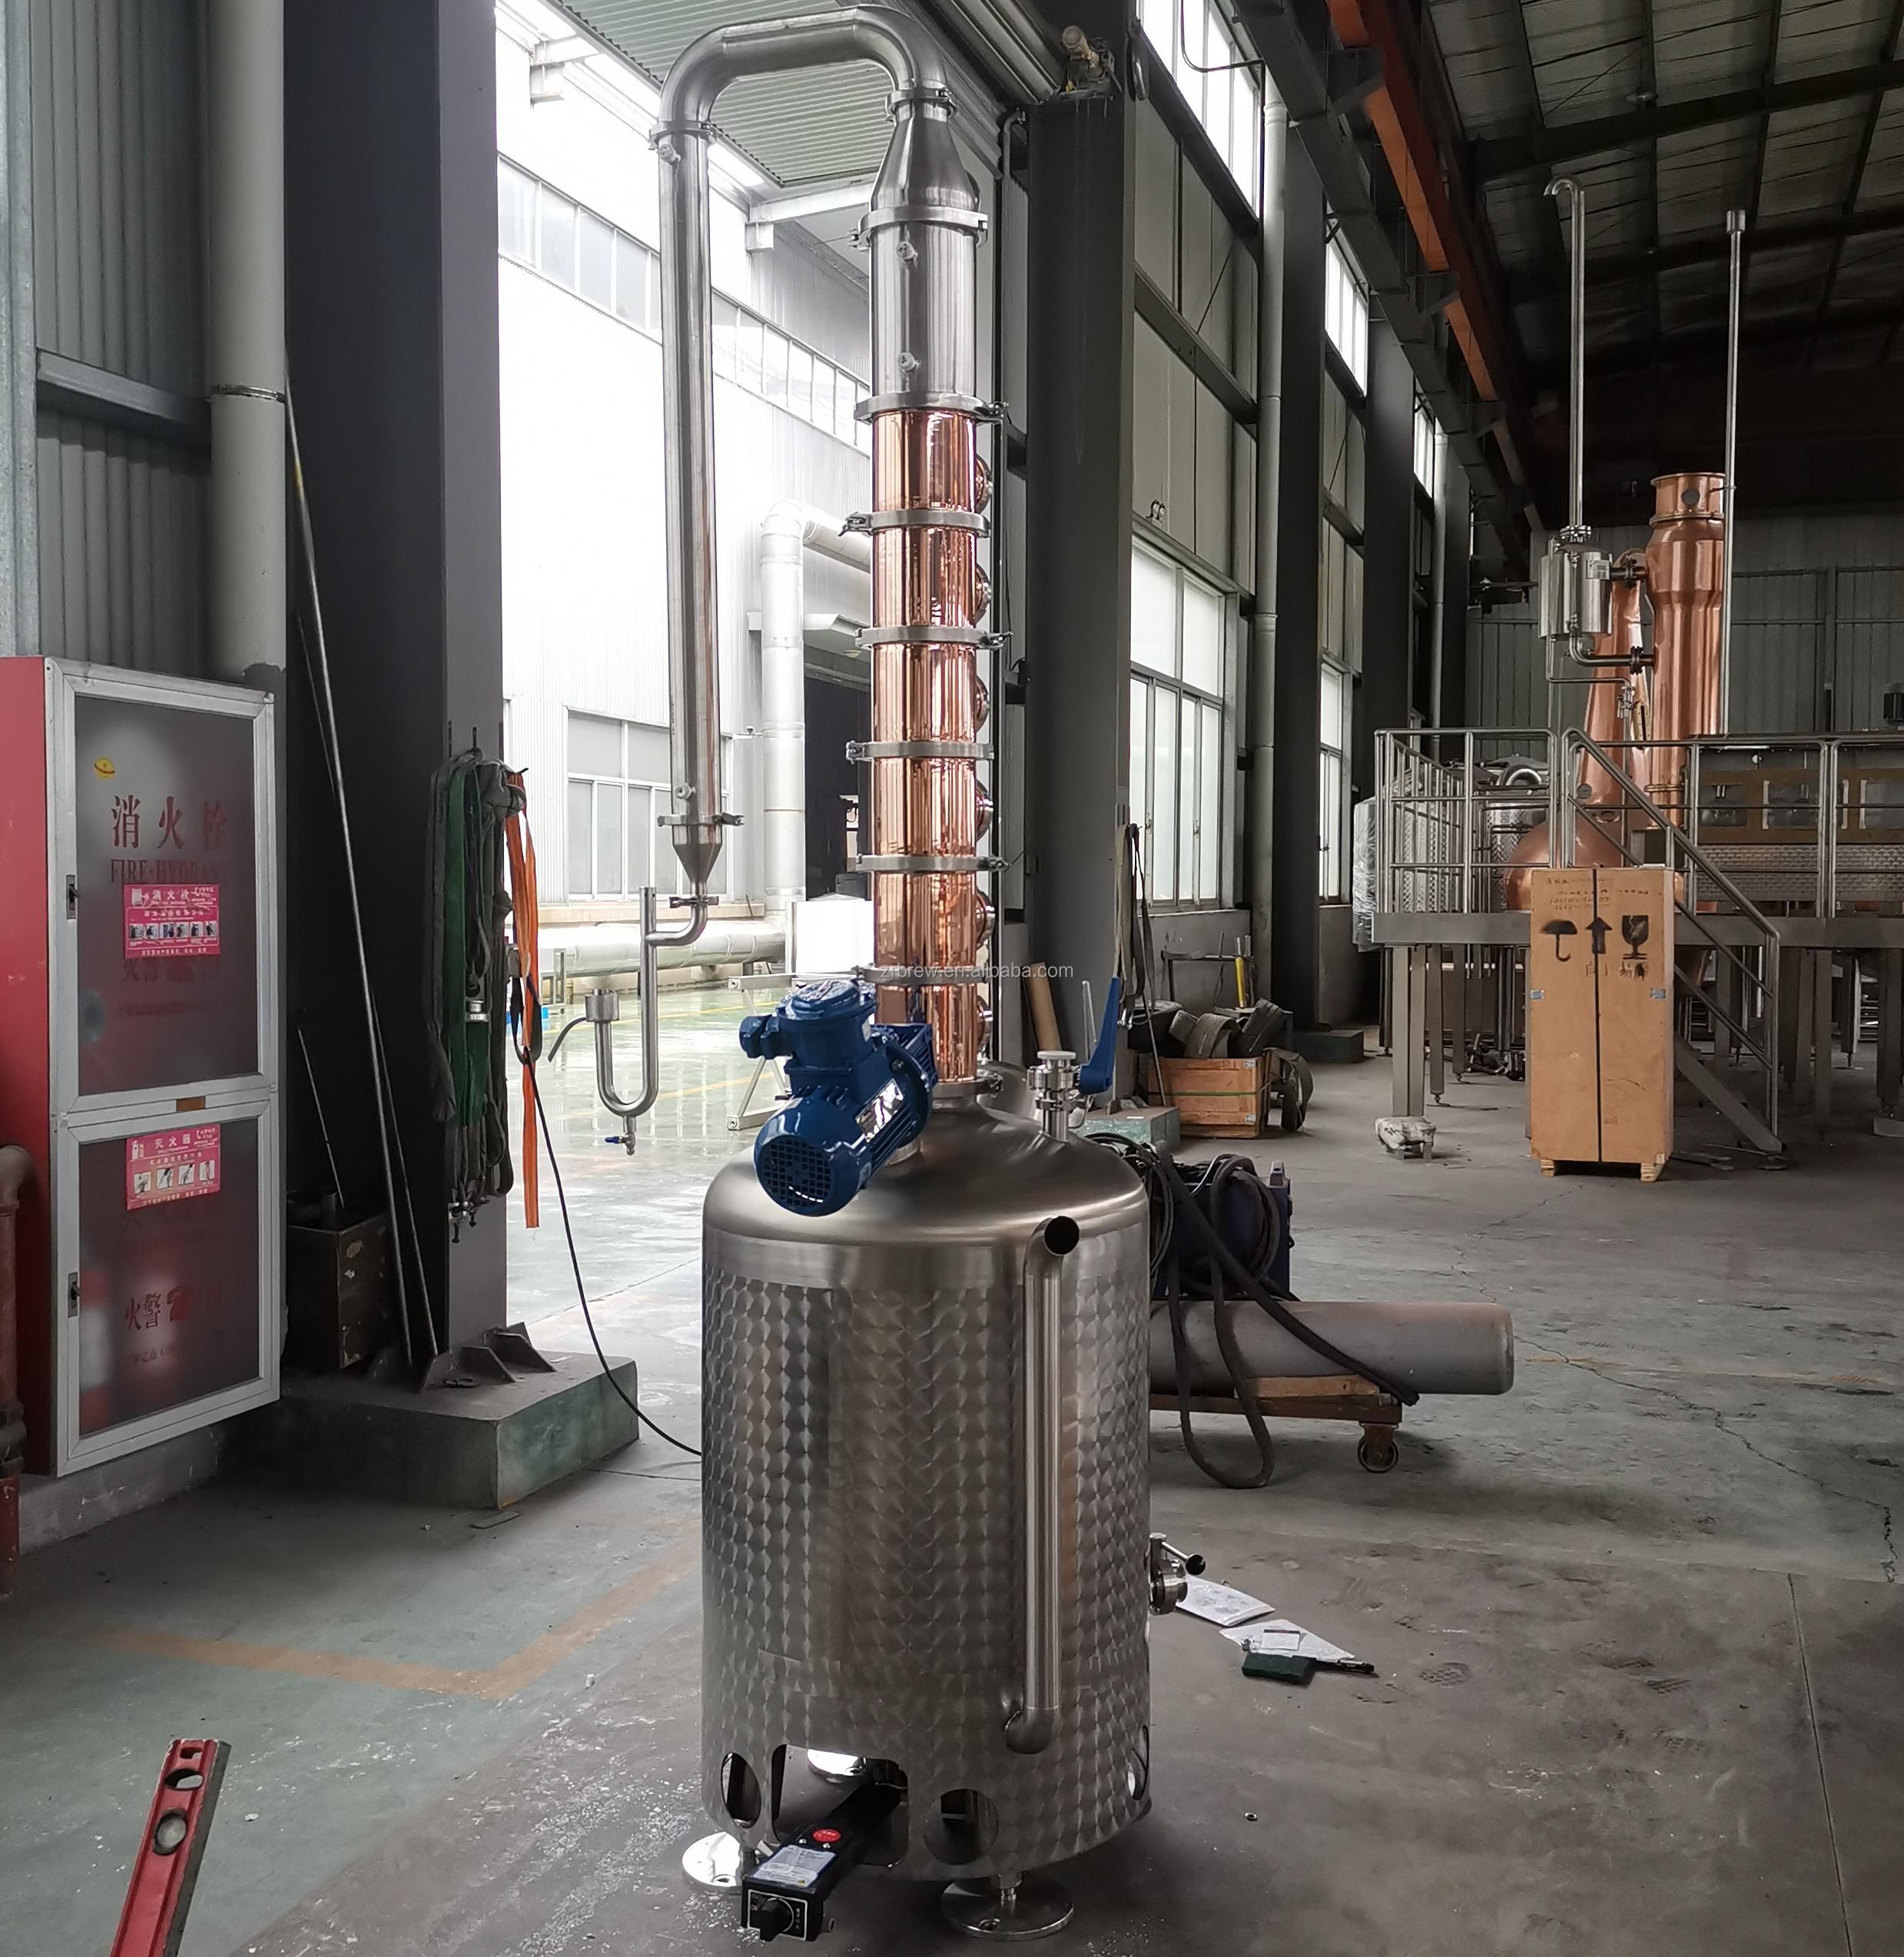
The 100L Column Still features a hybrid build that maximizes whiskey flavor and equipment durability. The boiler is crafted from diamond-embossed food-grade SUS304 stainless steel, equipped with a heavy-duty base and sight glass ports designed specifically for direct fire (gas or wood) heating. This method allows for rapid temperature rise and precise flame control, promoting the Maillard reaction for deeper, more complex grain flavors. The fractioning column is made of high-purity copper, which triggers natural catalytic reactions and effectively removes unwanted sulfur compounds, bringing a smooth and layered taste to your whiskey.
Multi-Plate Copper Column for Whiskey Distillation
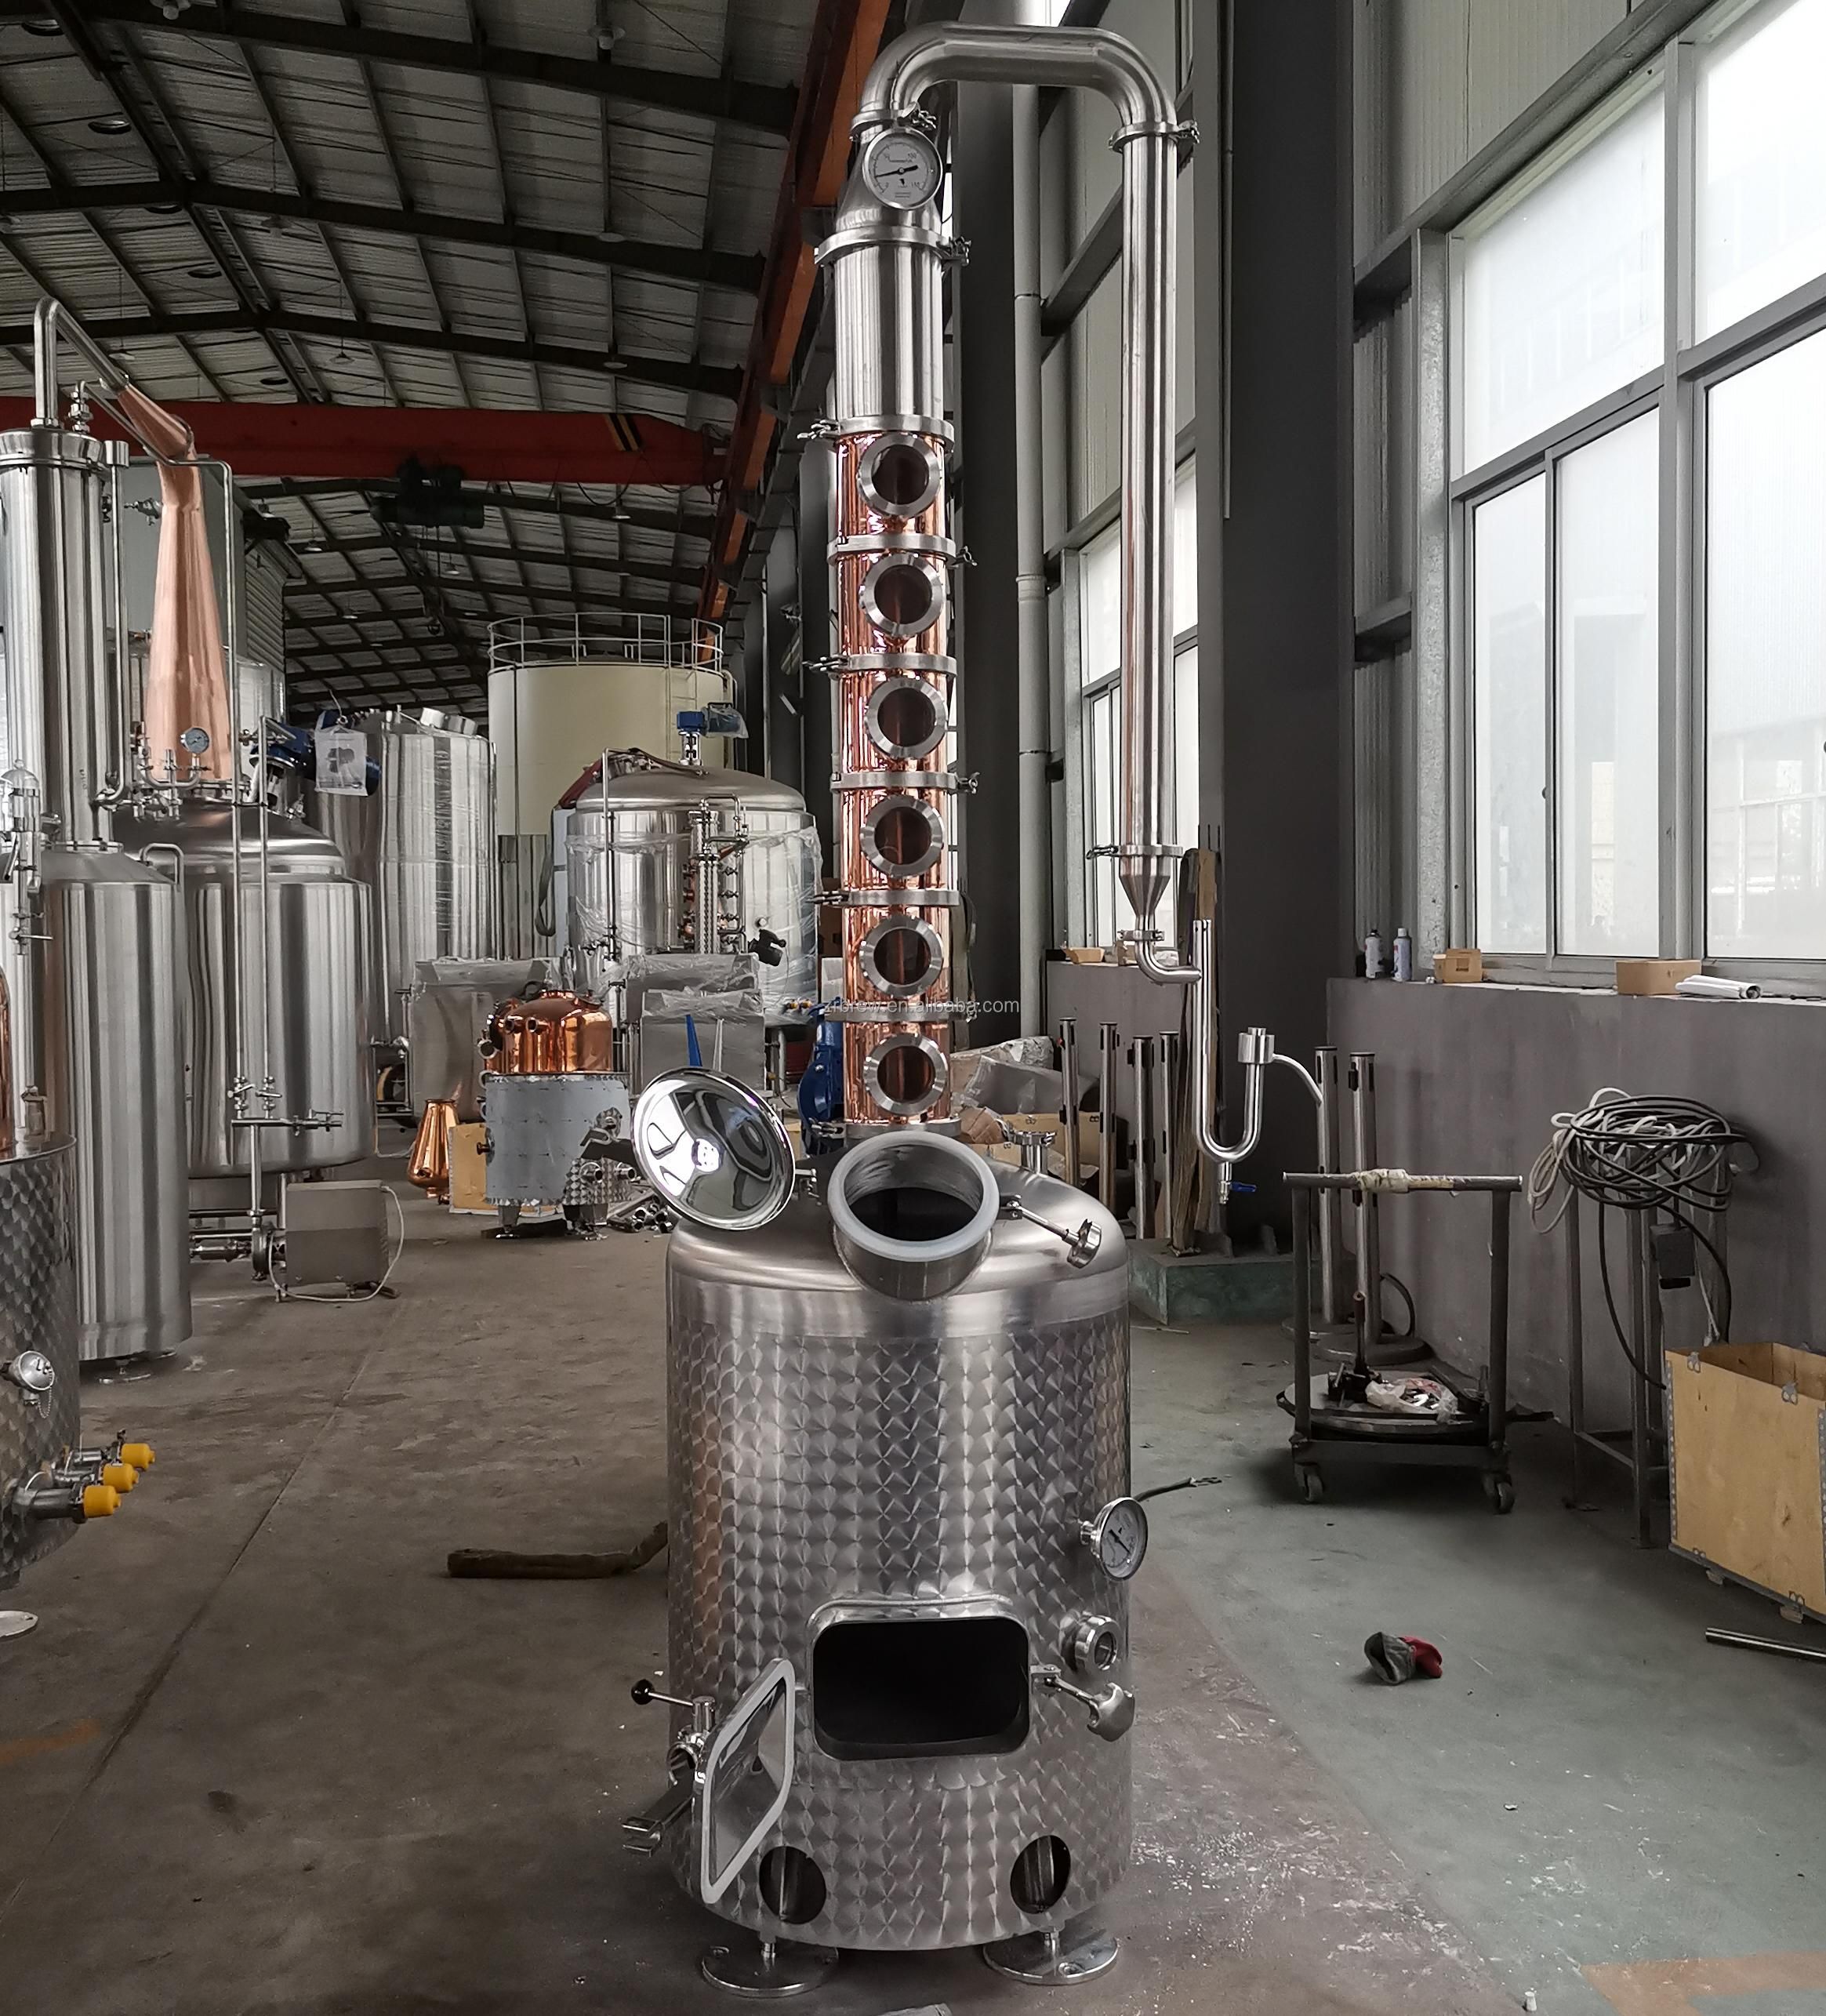
At the heart of the 100L Column Still is its multi-plate copper fractioning column fitted with sight glass windows. This column design achieves controllable fractional distillation and stable internal reflux. Heavy vapors condense and flow back to the boiler, while refined alcohol vapors rise upward to the condenser, helping you separate cuts precisely and get a cleaner whiskey distillate.
Efficiency, Visibility & Easy Maintenance
The 100L Column Still is designed for hands-on whiskey distilling operation. Sight glass ports on the copper column allow real-time observation of vapor and reflux status. A pressure gauge monitors working pressure continuously, and the sampling port enables easy distillate testing during whiskey runs. The bottom features a large quick-opening manway and a discharge valve, which simplifies waste liquid draining and makes cleaning exceptionally easy. Flange connections are detachable for thorough internal maintenance, making this direct-fire still a practical and reliable option for small-batch whiskey production.
ZR BREW is a leading manufacturer of brewing, distilling, winemaking, and kombucha fermentation equipment with 14 years of industry expertise. We are dedicated to our high-end product line and uphold the craftsman spirit to deliver first-class brewing solutions. With a strong reputation for quality and reliability, we have established partnerships with clients across more than 40 countries worldwide.
| Model | ZR-DT-100L |
| Capacity | Effective volume: 100L |
| Material | SUS304 SUS316 Red Copper |
| Uasge | Whisky |
| Application | Home commercial |
| Heating way | Electric heating Steam heating Direct fire heating |
| Control System | Fully automated with PLC Siemens Semi-Automated with PID Schneider |
| Voltage | Three-phase/380(220, 415,480…)v/50(60)Hz Single phase/220(110, 240…)v/50(60)Hz |
| Note:1Barrel (BBL) =117 Liter 1Hl=100 Liter 1Gallon=3.7854 Liter | |
Types | Volume | Component |
Whisky distiller | 50-5000L | Still pot, swan neck, condenser, CIP, pipe system |
Vodka distiller | 50-5000L | Still pot , onion head, column, dephlegmator, condenser, pipe system |
Brandy distiller | 50-5000L | Still pot, onion head, dephlegmator, column, condenser ,CIP, pipe system |
Rum distiller | 50-5000L | Still pot, column, condenser, CIP, pipe system |
Gin distiller | 50-5000L | Still pot, column, gin basket, condenser, CIP, pipe system |
Multi-spirits distiller | 200-5000L | Still pot, onion head, dephlegmator, column, gin basket, condenser, CIP, collecting tank |
1. Material & Craftsmanship
· Brazed Copper Distillation Tower: The column is constructed from premium-grade copper with precision-brazed joints, ensuring exceptional airtightness and durability. The copper material actively interacts with whiskey vapors, catalyzing the removal of unwanted sulfur compounds and promoting the development of a sweet, fruit-forward, and complex malt profile.
· Heavy-Duty Hammered SUS304 Boiler: The 100L boiler features a robust, diamond-hammered 304 stainless steel body. This textured exterior not only provides an elegant, professional aesthetic but also significantly enhances structural rigidity and scratch resistance. The thick-walled design ensures superior heat retention for direct-fire heating, minimizing thermal stress on the vessel.
· Full Food-Grade Construction: All internal components, including the vapor path and the reflux line, are manufactured from food-grade stainless steel and copper. This guarantees zero chemical leaching, ensuring the absolute safety and purity of the distilled spirits while making the interior easy to clean and maintain.
2. Functional Design
· Direct-Fire Heating Capability: Specifically engineered for direct-fire (gas/LPG) applications, the reinforced boiler base is designed to withstand high-intensity heat. The direct thermal input creates vigorous boiling and a rolling convection current, facilitating a natural "Maillard reaction" on the bottom for a richer, toasted-oak and caramelized flavor profile typical of traditional whiskey production.
· Multi-Sight-Glass Observation Column: The copper tower is equipped with multiple round sight glasses (as shown in the image) at every stage. This allows distillers to visually monitor vapor flow, "flooding" (liquid holdup), and the active bubbling state in real time, enabling precise control over the distillation speed and cut points (Foreshots, Hearts, Feints).
· Optimized Curved Vapor Arm & Airtight Seals: The top section features a smooth, 90-degree curved vapor arm that directs the rising spirit into the condenser without creating turbulent back-pressure. Bolted flanged connections with food-grade silicone gaskets ensure a completely vapor-tight seal, preventing valuable alcohol loss during the run.
· Gravity-Fed Condenser with Sight Glass: The horizontally mounted stainless steel coil condenser utilizes efficient gravity-fed vapor flow, allowing for rapid and complete condensation of the vapor. A built-in pressure-relief valve (or vacuum breaker on top) ensures safe operation, while the integrated alcohol sight glass (the small glass piece below the condenser) allows the distiller to visually check the clarity and flow rate of the output spirit in real time.
· Precision Temperature & Pressure Monitoring: Strategically placed dial thermometers on both the top column and the boiler body, combined with the bottom drain valve and easy-access manway, deliver comprehensive process control. The large front manway provides effortless loading of grain wash and easy cleanup of spent solids after each distillation run.
What is the capacity of the 100L Column Still for Whiskey Distillation (Direct Fire)?
The 100L Column Still for Whiskey Distillation (Direct Fire) features a 100-liter boiler capacity. With the recommended 70-80% fill rate, you can process 70-80L of wash or mash per batch, yielding approximately 10-20L of high-proof spirit per run.
What makes the direct fire heating version different from electric models?
The 100L Column Still for Whiskey Distillation (Direct Fire) differs from electric models in several ways: - Uses gas (propane/natural gas) burner instead of electric elements - Provides more traditional heating method favored by some distillers - Can produce slightly different flavor profile due to heat distribution - No electrical requirements (ideal for off-grid locations) - Lower operating cost in areas with cheap gas - Traditional moonshine still design
What type of burner is used for the 100L Column Still for Whiskey Distillation (Direct Fire)?
The 100L Column Still for Whiskey Distillation (Direct Fire) can use: - Propane (LP gas) burner: most common for mobile or outdoor operations - Natural gas burner: for fixed installations with gas supply - Butane burner: alternative option - The still includes a burner mounting area at the bottom - Adjustable flame control for temperature management - Burner not typically included (sold separately to allow customer choice)
Can I control the alcohol proof with the 100L Column Still for Whiskey Distillation (Direct Fire)?
Yes. The 100L Column Still for Whiskey Distillation (Direct Fire) offers multiple proof control options: - Use all plates for maximum proof (90-95% ABV) - Bypass some plates for lower-proof, more flavorful spirits - Traditional cut management (foreshots, heads, hearts, tails) - Parrot/spout for real-time ABV monitoring - Flame control affects distillation speed and proof - Can produce everything from 40% ABV to 95% ABV
What utilities do I need for the 100L Column Still for Whiskey Distillation (Direct Fire)?
The 100L Column Still for Whiskey Distillation (Direct Fire) requires: - Gas supply: propane tank or natural gas line - Cooling water: continuous flow of 200-400 L/hour for condenser - No electricity required for heating (may need for pumps or controls) - Drainage: floor drain for cleaning and waste water - Proper ventilation: essential for safe gas combustion - Fire extinguisher and safety equipment
Shandong Zeren Machinery Equipment Co., Ltd. is an equipment manufacturer focusing on biological fermentation industry
Copyright © Shandong Zeren Machinery Equipment Co., Ltd. All Rights Reserved |
Sitemap
| Technical Support: